Table of Contents↓
The Art and Science of Food Recipe Formulation: Balancing Taste, Nutrition, Shelf Life and Cost
A food concept can sound simple on paper: a snack with more protein, a sauce with less sodium, a ready meal with a longer shelf life, or a baked product that delivers familiar indulgence with a better nutritional profile. Turning that concept into a repeatable commercial product requires much more than combining ingredients until the flavour seems right.
Food recipe formulation is the structured process of selecting, combining and testing ingredients against defined targets for taste, texture, nutrition, safety, shelf life, manufacturing performance and cost. These targets are connected. Reducing sugar may affect browning, moisture and mouthfeel. Replacing fat can alter flavour release and structure. Adding protein may create chalkiness, sedimentation or a firmer texture. Extending shelf life may require changes to pH, water activity, processing or packaging.
The most effective formulations are therefore developed as integrated systems. A recipe that performs well in a kitchen trial may fail during production, while a formula that meets a nutrition target may not satisfy consumers. Successful development brings sensory, technical, regulatory and commercial decisions together before the product reaches scale.
What food recipe formulation involves
Food recipe formulation begins with a product brief. The brief should define the intended consumer, format, serving size, pack size, target markets, positioning, nutritional claims, expected shelf life, manufacturing route and target cost. It should also identify non-negotiable requirements, such as allergen exclusions, halal suitability, vegan status, organic positioning or restrictions on particular additives.
This early definition prevents a common development problem: optimising one attribute while discovering later that the product cannot be manufactured economically or labelled as intended. A formulation designed for chilled distribution may use a different preservation and packaging strategy from one intended for ambient export. A product sold across several markets may use a common base recipe, but still require adjustments to ingredients, claims, flavour intensity or label declarations.
The main technical objectives usually include:
- Flavour, aroma and overall sensory acceptance
- Texture, viscosity, structure and eating quality
- Nutritional composition and serving-based targets
- Microbiological and physical stability
- Compatibility with the intended process and packaging
- Reliable ingredient supply and acceptable unit cost
- Consistent quality during production and distribution
These objectives should be prioritised rather than treated as equal in every product. For example, a premium dessert may accept a higher ingredient cost to protect texture, while a high-volume staple may require a tighter cost ceiling and a more flexible ingredient system.
From product brief to working recipe
A disciplined food product development process normally moves through concept definition, ingredient research, bench formulation, sensory review, analytical testing, pilot production, validation and commercial scale-up. The stages may overlap, but skipping one often transfers risk to a later and more expensive stage.
Define the product architecture
Before selecting individual ingredients, the development team should understand the product’s architecture. A sauce may depend on an emulsion, a suspension, an acidified base or a starch-thickened system. A baked product may depend on gluten development, gas retention, fat crystallisation and moisture migration. A snack may require control of expansion, fracture, oil uptake and seasoning adhesion.
This definition determines which ingredients are doing structural work and which are primarily contributing flavour, colour or nutrition. It also helps establish an order of addition and a suitable processing sequence.
Choose ingredients by function, not only by label appeal
Ingredients are often selected for several reasons at once. An oat ingredient may contribute flavour, solids and viscosity. A dairy or plant protein may add nutrition but also influence water binding, opacity and texture. An acidulant can provide sourness, lower pH and support microbial control. A hydrocolloid may improve suspension or mouthfeel, but excessive use can create a slimy or gummy perception.
Understanding ingredient functionality in food formulation is particularly important when a familiar ingredient is removed or replaced. Substitution is rarely one-to-one. Replacing sucrose with a high-intensity sweetener may restore sweetness but not bulk, browning, freezing-point effects or body. Replacing butter with a lower-fat system may require changes to emulsification, water management and flavour delivery.
A practical formulation record should document each ingredient’s purpose, inclusion rate, specification, supplier status, allergen profile, regulatory considerations and potential alternatives. This creates a clearer basis for reformulation if cost, availability or market requirements change.
Balancing taste, texture and nutrition
Balancing taste and nutrition in food products requires more than reducing an undesirable nutrient. Consumers experience the entire product, so a lower-sugar, lower-sodium or higher-protein formula must still deliver the expected flavour, aroma, texture and satisfaction.
Sweetness and sugar reduction
Sugar contributes sweetness, bulk, colour development, moisture retention and texture. In bakery products, it affects spread, tenderness and browning. In sauces and beverages, it can soften acidity and reduce the perception of bitterness. Removing it may therefore expose sour, bitter or astringent notes even when sweetness is replaced.
Formulators may need a combination of sweetening systems, flavour adjustment, bulking ingredients, fibres or process changes. The right approach depends on the product category and the claim being pursued. A formula that uses less added sugar may still need careful control of total sugars and serving size for labelling purposes.
Protein, fibre and fortification
Increasing protein or fibre can improve nutritional value, but these ingredients often affect texture and flavour. Protein powders may create dryness, grittiness or a lingering aftertaste. Fibres can increase viscosity, bind water or produce a dense structure. Minerals may introduce metallic notes or interact with colour and stability systems.
Nutritional optimization in recipe development works best when the nutrition target is considered alongside the product’s physical structure. The team should assess ingredient form, particle size, hydration, heat sensitivity and interactions with other components. A nutritional analysis should be performed using the intended ingredient specifications rather than generic database values alone wherever possible.
Sodium and fat reduction
Sodium contributes more than saltiness. It can influence flavour intensity, protein behaviour, preservation and overall balance. Reducing it may require stronger use of herbs, spices, acids, umami ingredients or aroma. Fat contributes richness, lubrication, flavour release and structure, so reducing it can make a product seem dry or thin.
These changes should be assessed through sensory testing rather than assumed to work from a formulation spreadsheet. Small changes in particle size, serving temperature or processing can alter perceived intensity significantly.
Sensory evaluation is a development tool
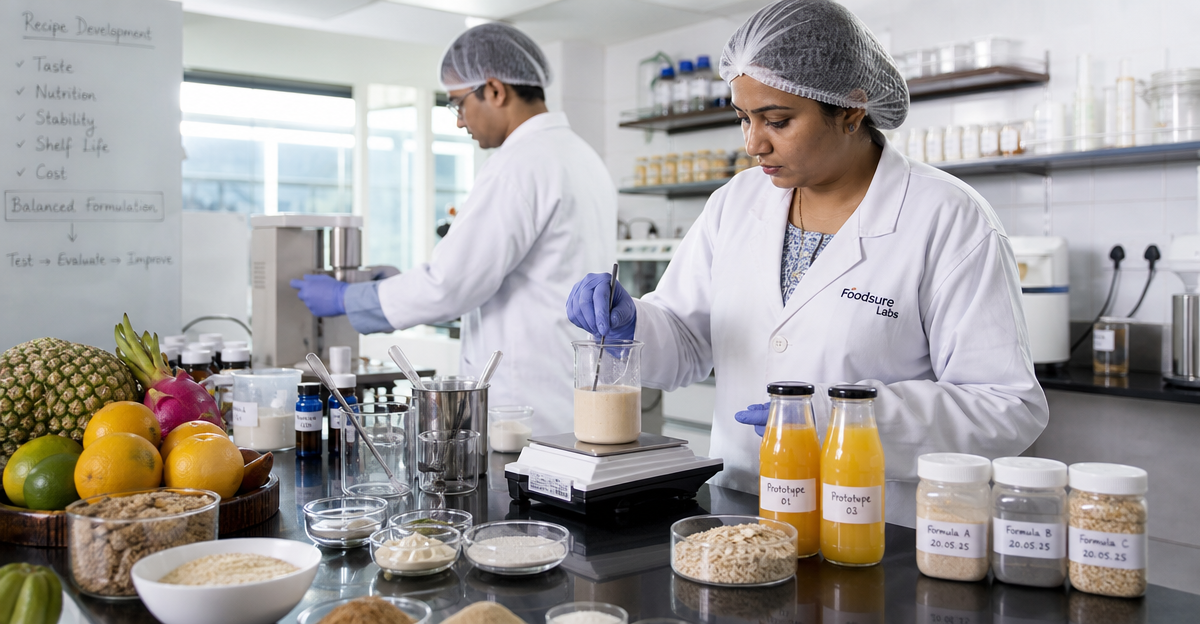
Sensory evaluation for food products helps determine whether a technically acceptable recipe is also acceptable to its intended users. Sensory work should begin early, not only after the formula appears finished.
Simple internal reviews can compare prototypes for sweetness, saltiness, acidity, aroma, aftertaste, mouthfeel, firmness, juiciness, colour and overall liking. More structured testing may be appropriate when the team needs to identify a preferred formula, compare a product with a benchmark or understand why a prototype is being rejected.
Testing conditions need control. Samples should be coded, served consistently and evaluated under suitable temperature and storage conditions. The team should distinguish between preference and diagnosis. A panel may prefer one sample, but technical questioning is needed to identify whether the difference comes from flavour intensity, texture, aftertaste, appearance or another attribute.
Consumer expectations also vary between markets. A common base formulation may be practical for products with broadly familiar flavour profiles, while stronger localisation may be needed for sweetness, heat, acidity, seasoning intensity or texture. Market adaptation should be based on a clear commercial reason rather than creating unnecessary versions.
Designing for shelf life and food safety
Food shelf life formulation is the process of developing a product that remains safe and acceptable for the intended period under defined storage and distribution conditions. Shelf life is not determined by one ingredient or one test.
Key variables may include pH, water activity, moisture migration, oxygen exposure, oxidation, microbial growth, light, temperature, packaging permeability and handling after production. A product can remain microbiologically safe while suffering unacceptable colour loss, rancidity, separation, staling or texture change.
Preservation decisions should be linked to the product’s risk profile and manufacturing method. Possible controls include thermal processing, acidification, refrigeration, dehydration, suitable preservatives, hygienic processing and protective packaging. These measures must be assessed together because changing one can affect the others.
For example, lowering moisture may improve stability but create a harder texture. Increasing acidity may support microbial control but make the flavour too sharp. A stronger heat treatment may extend safety margins while damaging colour, nutrients or volatile flavour compounds.
Food safety and HACCP planning should be connected to formulation and process development. The team should identify hazards, control points, ingredient risks, allergen controls and conditions that could change during scale-up. Shelf-life claims should be supported by an appropriate study using representative packaging, realistic storage conditions and defined acceptance criteria.
Cost-effective recipe development without sacrificing performance
Cost-effective recipe development starts with a target cost, not a calculation made after the formula is complete. The target may be expressed per kilogram, serving, pack or finished case, depending on the commercial model.
Ingredient price is only one part of cost. Yield loss, waste, water absorption, processing time, labour, energy, packaging, minimum order quantities, storage requirements and supply reliability can all affect the final result. A lower-priced ingredient may be less economical if it causes higher wastage or requires a slower process.
Ingredient costing methods should allow the team to compare formulations at equivalent finished yield. This is especially important when ingredients have different solids content, potency or moisture levels. The costing model should also show the effect of inclusion-rate changes and supplier price movements.
Cost optimisation may involve:
- Reviewing high-cost ingredients and their actual functional contribution
- Comparing equivalent grades or formats from approved suppliers
- Improving yield and reducing process losses
- Using a blend of ingredients rather than relying on one expensive component
- Designing specifications that allow reliable, commercially available materials
- Reducing unnecessary complexity in the recipe or process
Substitution trials should assess sensory quality, nutrition, stability and processing, not cost alone. A formula that is cheaper on paper can become more expensive if it creates inconsistent batches or shortens shelf life.
Moving from bench recipe to commercial production
A bench formula does not automatically translate to a factory. Mixing intensity, vessel geometry, heating rate, shear, hold time, filling temperature and cooling behaviour can all change the finished product.
Scaling recipes for production requires process parameters as well as ingredient percentages. The development record should specify order of addition, hydration time, mixing speed, temperature limits, pH adjustment points, filtration or homogenisation requirements and acceptable process tolerances.
Pilot trials are useful because they expose problems that are difficult to see at bench scale. A powder may disperse quickly in a small beaker but form lumps in a larger vessel. A sauce may emulsify under laboratory shear but separate during transfer. A baked product may have a different moisture gradient when the oven load and airflow change.
Commercial food recipe development should therefore include at least one representative production trial where possible. Samples from the beginning, middle and end of the run can be compared for weight, texture, colour, pH, moisture, fill accuracy and sensory quality. The goal is not merely to produce a successful batch, but to understand the operating window that produces consistent batches.
Regulatory, labelling and international market considerations
Regulatory requirements vary by market and should be checked before launch. Ingredient permissions, additive declarations, allergen statements, nutrition panels, claims, fortification rules and language requirements may differ between jurisdictions.
A global product strategy does not always require a different recipe for every market. A common formulation may work where the ingredient system, sensory profile, claims and manufacturing route are acceptable across the intended markets. Localisation becomes more likely when a particular ingredient is restricted, unavailable, difficult to certify, poorly understood by consumers, unsuitable for local taste expectations or incompatible with a required claim.
Halal suitability may also be relevant for products intended for Muslim-majority or internationally distributed markets, but the specific requirements should be confirmed with the appropriate certification and regulatory bodies. Ingredient source, processing aids, flavour carriers and shared manufacturing equipment may need review.
Label development should begin before the final recipe is approved. A change in sweetener, compound ingredient, fortificant or flavour system can affect allergen declarations, ingredient order, nutrition values and permitted claims. Early review reduces the risk of developing a product that requires expensive reformulation late in the process.
Testing before commercialisation
Before launch, the formula should be assessed against the original brief and its manufacturing conditions. Typical activities include:
- Sensory comparison and acceptance testing
- Nutritional analysis and label calculation
- Microbiological and chemical safety assessment
- Accelerated or real-time shelf life testing, where appropriate
- Packaging compatibility and seal or closure checks
- Pilot or factory production trials
- Review of specifications, claims and market-specific labelling
Shelf life testing should use the proposed pack and realistic distribution conditions. Testing only the recipe in a laboratory container may overlook oxygen transfer, light exposure, seal performance or moisture migration in the commercial package.
When a product shows instability, reformulation should be guided by the failure mode. Separation may point to emulsification, particle size, viscosity or processing. A stale flavour may involve oxygen, fat quality or packaging. Texture loss may relate to moisture movement, temperature abuse or ingredient interaction. Diagnosing the mechanism is more efficient than making unrelated changes to several ingredients at once.
Building a reliable formulation record
A strong technical file makes the product easier to manufacture, audit and reformulate. It should include the approved recipe, ingredient specifications, supplier information, process instructions, critical limits, testing methods, sensory criteria, packaging details, shelf-life evidence and change-control history.
The document should distinguish between a target and a tolerance. “Mix until smooth” is less useful than defining the mixing conditions and the visual or analytical standard for acceptance. Similarly, a pH target should be accompanied by an acceptable range and a clear measurement method.
FoodSure can support businesses that need assistance with formulation, nutritional optimisation, sensory review, shelf-life assessment, pilot trials or preparation for commercial manufacture. The appropriate level of support depends on whether the project needs a new recipe, a reformulation, technical troubleshooting or a route from prototype to production.
Conclusion
Effective food recipe formulation connects consumer expectations with measurable technical and commercial requirements. Taste cannot be separated from texture, nutrition from ingredient functionality, or shelf life from processing and packaging. Cost control also needs to consider yield, consistency and supply risk rather than ingredient price alone.
A well-managed development programme defines the brief early, selects ingredients for their complete function, tests sensory and nutritional performance, validates shelf life and proves the process at representative scale. For products intended for international markets, the formulation should be designed with regional regulation, availability, labelling and taste expectations in view without creating unnecessary complexity. That combination gives a recipe a better chance of becoming a safe, consistent and commercially viable food product.
Frequently Asked Questions
What is food recipe formulation?
Food recipe formulation is the structured process of selecting and combining ingredients to achieve defined targets for flavour, texture, nutrition, safety, shelf life, consistency and cost. It includes recipe design, testing, refinement and preparation for manufacture.
How do you balance taste and nutrition in a food recipe?
Start by defining the nutritional targets, then select ingredients that support flavour and texture while controlling sugar, sodium, saturated fat and calories. Sensory testing and nutritional analysis are used together to refine the formula rather than relying on nutrient calculations alone.
Why is ingredient functionality important in recipe formulation?
Ingredients contribute more than flavour. They can affect structure, emulsification, moisture retention, texture, stability, colour, processing performance and shelf life. Understanding these functions helps prevent failures when an ingredient is reduced, removed or replaced.
How can recipe formulation improve food shelf life?
Shelf life can be improved by controlling water activity, pH, oxidation, microbial growth, processing conditions, packaging and storage requirements. The chosen controls must be validated through appropriate shelf-life testing using the intended product and pack.
How do formulators control the cost of a food product?
Cost is managed by setting a target cost per serving or unit, comparing ingredient prices, optimising inclusion rates, reducing process waste, selecting dependable suppliers and testing suitable alternatives. Yield and manufacturing efficiency should be included in the calculation.
What testing is needed before commercialising a food recipe?
Typical testing includes sensory evaluation, nutritional analysis, food safety assessment, stability and shelf-life testing, packaging compatibility checks, pilot-scale production and regulatory label review. The exact programme depends on the product category and intended markets.
Can one food formulation be sold in multiple international markets?
Yes, a common base formulation can be practical when the ingredients, sensory profile, claims, labelling and manufacturing requirements are acceptable across those markets. Localised versions may be needed when regulations, ingredient availability or consumer expectations differ materially.
Why can a successful kitchen recipe fail during factory production?
Factory equipment changes mixing, heating, shear, transfer and cooling conditions. Ingredient hydration and dispersion may also behave differently at larger volumes. Pilot production helps identify these differences and establish process parameters before full-scale manufacture.
When should shelf-life testing begin?
Shelf-life testing should begin once the formulation, process and proposed packaging are sufficiently representative of the commercial product. Testing an early prototype can provide useful direction, but final claims should be based on the intended recipe and pack.
What information should a commercial formulation file contain?
It should contain the approved recipe, ingredient specifications, supplier details, process instructions, critical limits, testing methods, sensory standards, packaging information, shelf-life evidence, label data and change-control records. This supports consistent manufacturing and future reformulation.