Table of Contents↓
The Art and Science of Food Recipe Formulation: Balancing Taste, Nutrition, Shelf Life and Cost
A successful food product is rarely the result of simply combining good ingredients. A recipe must perform under practical conditions: it needs to taste appealing, deliver the intended nutritional profile, remain safe and stable throughout its shelf life, run consistently in production and meet a viable cost target. These requirements often compete with one another. Reducing sugar can affect texture and browning. Replacing fat may change flavour release and mouthfeel. Extending shelf life can require processing or packaging changes that increase cost.
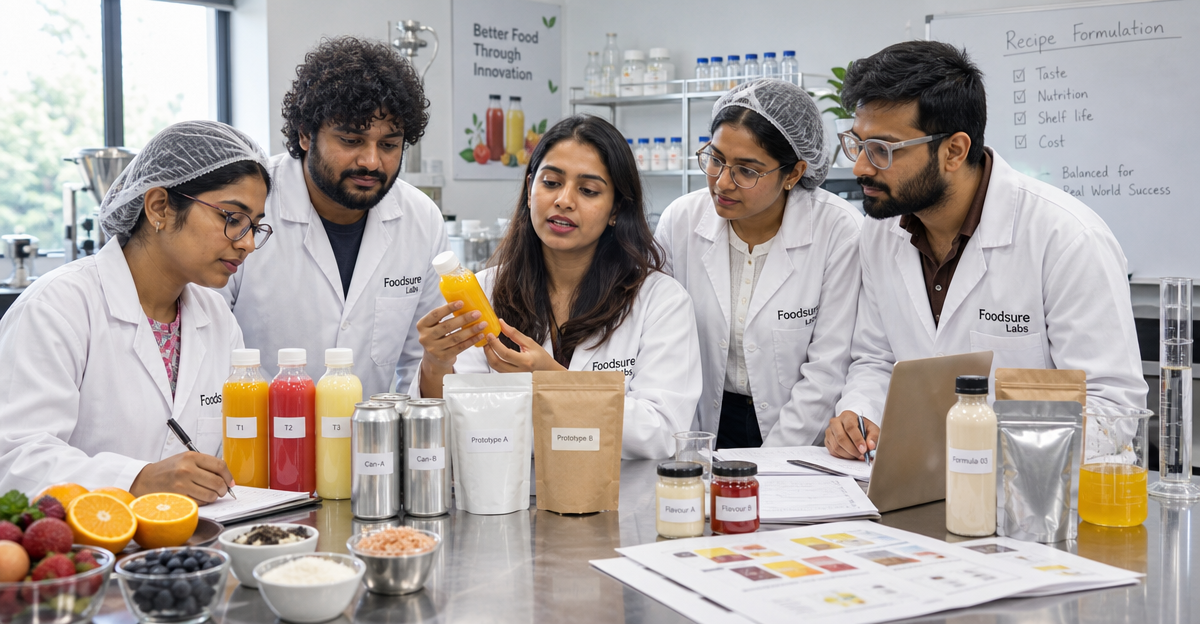
Food recipe formulation provides a structured way to manage these trade-offs. It converts a product concept into a measurable formula by defining ingredient levels, processing conditions, quality targets and testing requirements. Whether the product is a ready meal, sauce, snack, bakery item, dairy alternative or functional food, formulation decisions made early influence manufacturing, labelling, procurement and commercial performance later.
What food recipe formulation involves
Food recipe formulation is the structured process of selecting, combining and optimising ingredients to create a product that meets targets for taste, texture, nutrition, safety, shelf life, manufacturability and cost. It goes beyond writing a recipe for a kitchen. A commercial formula must be repeatable, scalable and supported by specifications that allow different production batches to deliver a consistent result.
The process usually begins with a product brief. This may define the intended consumer, eating occasion, pack format, nutritional claims, target retail price, serving size, manufacturing route and markets in which the product will be sold. A product intended for chilled retail will have different technical priorities from an ambient sauce. A high-protein snack will present different texture and flavour challenges from a reduced-sugar beverage or a fortified bakery product.
From the brief, the development team translates broad ambitions into measurable requirements. Examples include:
- Target calorie, protein, fibre, sugar, sodium or fat levels
- Desired texture, viscosity, crispness, firmness or spreadability
- Required pH, water activity or moisture range
- Minimum shelf life under defined storage conditions
- Acceptable ingredient and manufacturing cost
- Processing, packaging and distribution constraints
- Labelling, allergen and regulatory requirements in the target market
These targets create a framework for the recipe formulation process. Without them, development can become an endless cycle of subjective adjustments. A product may taste good in a single kitchen trial but fail when produced at scale, stored for several weeks or assessed against its intended cost.
Start with the product brief, not the ingredient list
Many development projects begin with a preferred ingredient or a prototype. That can be useful for inspiration, but it is not enough to define a commercial product. The same ingredient may behave differently depending on its concentration, particle size, processing history, pH, moisture level and interactions with other components.
A practical brief should answer several questions before detailed formulation begins:
- What product experience should the consumer receive?
- Where and how will the product be stored?
- Will it be manufactured in-house, through a co-manufacturer or in a commercial kitchen?
- What equipment and processing steps are available?
- What claims or nutritional targets are required?
- Which ingredients are acceptable from a cost, sourcing, allergen and market-access perspective?
This stage is closely connected to the wider food product development process. A formulation that depends on an uncommon stabiliser, a fragile botanical extract or a specialist processing step may be technically possible but commercially unsuitable if supply is inconsistent or manufacturing partners cannot handle it.
Balancing taste, texture and nutrition
Balancing taste and nutrition is rarely achieved by removing one ingredient and replacing it with a direct equivalent. Sugar, fat and salt contribute more than flavour. They also affect bulk, water binding, viscosity, browning, crispness, aroma release and overall satiety.
Reducing sugar in a baked product, for example, may produce a less moist or less browned result. A lower-fat sauce may feel thin and release flavour differently. Sodium reduction can make acidity, bitterness or certain spices more noticeable. Protein and fibre additions may create dryness, grittiness or undesirable aftertaste if they are not incorporated into a suitable ingredient system.
Formulators therefore need to assess the complete sensory effect of a nutritional change. Possible approaches include:
- Using complementary sweetener or flavour systems rather than relying on one replacement ingredient
- Adjusting acidity, salt balance, aroma and spice to support a reduced-sugar or reduced-sodium profile
- Using fibres, starches, proteins or hydrocolloids to restore body and moisture
- Changing particle size or processing conditions to improve texture
- Rebalancing portion size while protecting the intended eating experience
A nutritionally improved formula is not automatically a successful one. If the product loses its expected flavour, texture or appearance, repeat purchase may suffer. Nutritional formulation should therefore be assessed alongside sensory acceptance, cost, stability and labelling implications rather than treated as a separate technical exercise.
Ingredient functionality matters as much as ingredient identity
Ingredients should be selected for what they do in the formula, not only for their name or marketing appeal. The same ingredient can perform several functions, while two ingredients with similar consumer descriptions may behave very differently during processing.
Ingredient functionality in food formulation can include water binding, emulsification, thickening, aeration, gel formation, crystallisation control, oxidation protection, flavour delivery, colour development and microbial control. Understanding these functions helps a development team predict what may happen when an ingredient is removed, substituted or reduced.
For example, a starch may provide viscosity during heating but lose performance under acid conditions. A protein may improve nutritional value while increasing water demand or creating a chalky mouthfeel. An oil may contribute richness but also affect emulsion stability and oxidation risk. A natural colour may satisfy a positioning requirement but show sensitivity to light, heat or pH.
Ingredient interactions are often more important than the performance of any single component. A formula may require staged addition, controlled hydration, a specific shear rate or a defined order of mixing. These details should be documented during development because a formula expressed only as ingredient percentages may not be sufficient to reproduce the intended result.
Designing for shelf life and product stability
Food shelf life optimization begins with identifying the main causes of deterioration. These may include microbial growth, oxidation, moisture migration, colour loss, flavour changes, texture breakdown, separation or chemical reactions between ingredients.
Different products fail in different ways. A crisp snack may absorb moisture and lose its texture. A sauce may separate or develop surface mould after opening. A high-moisture ready meal may experience microbial risks even when its sensory quality remains acceptable. A product containing oils, nuts or sensitive flavours may develop rancid notes through oxidation.
Key controls may include:
- pH and acidity management
- Water activity and moisture control
- Thermal processing or other validated preservation methods
- Oxygen reduction through packaging or processing
- Antioxidants, preservatives or protective ingredient systems where appropriate
- Barrier properties of the selected pack
- Storage temperature and distribution conditions
Shelf life cannot be established from the formula alone. Processing, filling, hygiene, packaging and storage all contribute to the final outcome. A formulation may remain stable in a small laboratory container but behave differently in a larger pack with more headspace, slower cooling or repeated consumer exposure after opening.
Relevant food preservation techniques should be evaluated against the product category and manufacturing route. The objective is not simply to extend shelf life as far as possible. Excessive processing may damage flavour, colour or texture, while a complex preservative system may conflict with the product’s positioning or labelling strategy.
Cost is a formulation variable, not a final calculation
Recipe cost optimization is more effective when it begins during concept development. Waiting until the final prototype is complete can force major substitutions that alter the product’s sensory and nutritional performance.
Basic recipe costing starts by multiplying the quantity of each ingredient by its purchase price. Commercial costing needs a wider view. It may include yield loss, trim, overfill, processing waste, labour, utilities, packaging, quality testing, warehousing and rejected batches. Ingredient prices may also vary according to minimum order quantities, seasonality, supplier location, import conditions and contract terms.
A useful ingredient cost analysis should examine both price and functionality. A more expensive ingredient may reduce the quantity of another component, shorten processing time or improve yield. Conversely, a lower-cost substitute may require additional stabilisers, longer mixing or more stringent quality control.
Cost reviews should consider:
- Cost per kilogram and cost per finished serving
- Expected production yield
- Ingredient losses during processing
- Packaging and secondary packing
- Labour and equipment requirements
- Quality, microbiological and shelf-life testing
- Supply continuity and approved alternative suppliers
The commercial target should be linked to the intended price architecture. A technically excellent formula may still require redesign if it cannot produce an acceptable margin at the expected selling price.
Turning a kitchen recipe into a manufacturable formula
A kitchen prototype is useful for exploring flavour and product direction, but it does not automatically translate into a factory process. Commercial equipment creates different shear, heat transfer, mixing patterns and residence times. Batch size can affect hydration, aeration, cooking uniformity and cooling speed.
During scale-up, the development team should document more than ingredient weights. The technical record may need to include addition order, mixing speed, mixing time, temperature profile, hold time, filling temperature, cooling rate and packaging conditions.
Equipment limitations can also require reformulation. A small batch may disperse a powder easily, while a larger vessel creates undissolved pockets. A sauce that pours correctly from a laboratory beaker may not pass through a commercial filling line. A bakery mixture may need a different deposit temperature or resting period when produced in larger quantities.
Commercial food recipe development should include pilot trials that reflect the intended production route as closely as possible. These trials can reveal whether the formula is tolerant of normal process variation and whether the target quality can be achieved without excessive manual intervention.
Useful scale-up questions include:
- Can ingredients be weighed and added consistently?
- Does the formula tolerate normal batch-to-batch variation?
- Are there risks of settling, foaming, scorching or blockage?
- Can the product be filled at the required speed and temperature?
- Does the packaging protect the product under expected distribution conditions?
- Can cleaning and allergen controls be managed effectively?
For smaller brands, commercial kitchen scaling may be the first bridge between bench development and industrial manufacturing. The same principle applies: equipment, batch size and process control must be considered before a formula is presented as production-ready.
Using sensory evaluation to make better decisions
Sensory evaluation for food products measures how people perceive flavour, aroma, appearance, texture, mouthfeel and overall liking. It provides evidence for decisions that might otherwise be based on the preferences of a small internal team.
Different methods answer different questions. A trained descriptive panel may help identify whether a product is too bitter, dry, acidic or dense. Consumer testing can indicate whether the target audience likes the product and how it compares with alternatives. Difference testing can establish whether a reformulated version is noticeably different from an existing product.
Testing should begin with clear objectives. If sugar is being reduced, the team may need to assess sweetness, aftertaste, mouthfeel and overall liking rather than asking only whether the product tastes good. If a protein ingredient is being changed, texture, dryness and aroma may be as important as nutritional composition.
Good sensory testing methods control sample preparation, serving order, storage conditions and evaluation criteria. Results should be considered alongside analytical data and cost information. A statistically preferred sample may still be unsuitable if it cannot be manufactured consistently or fails its shelf-life target.
Safety, labelling and international commercialisation
Food formulation must support safe production and accurate communication to the consumer. Ingredient declarations, allergen controls, nutrition information and permitted claims should be reviewed for each intended market. Regulatory requirements vary, so a formula and label that work in one jurisdiction may need adjustment elsewhere.
The development team should consider whether an ingredient has market-specific restrictions, whether naming conventions differ, and whether the proposed claim is supported by the finished product. Halal, kosher, vegan, organic or other positioning requirements may also affect supplier approval, processing controls and documentation, depending on the target market and product brief.
Food labeling and nutrition facts should be treated as part of formulation rather than a final artwork task. Ingredient levels determine declared nutrients, allergens and sometimes the wording that can be used on pack. A late substitution may change the nutrition panel or require a new regulatory review.
Food safety controls should be linked to the actual process. A HACCP review may identify hazards associated with raw materials, cooking, cooling, filling, storage or cross-contact. The formula, process and sanitation programme must work together; no ingredient adjustment can compensate for an uncontrolled critical step.
Common formulation challenges and how to manage them
Food formulation challenges usually arise from competing targets rather than a single technical error. Common examples include:
- Improving nutrition while protecting taste and texture
- Extending shelf life without excessive processing
- Replacing an ingredient without losing its functional role
- Meeting a cost target while maintaining quality
- Using natural or recognisable ingredients without compromising stability
- Developing one base formula for multiple markets
- Moving from a flexible laboratory process to controlled manufacturing
These problems are easier to manage when the team defines which product attributes are fixed and which can change. For example, a brand may require a specific allergen-free status and cost target but allow moderate adjustment to sweetness or colour. Another product may require a precise nutritional claim while accepting a different texture.
For international products, a common base formulation may be practical when ingredient permissions, taste expectations, labelling rules and supply conditions align. Localisation becomes more likely when sweetness preferences, permitted additives, pack sizes, climate exposure, certification requirements or ingredient availability differ materially. The decision should be based on technical and commercial evidence, not an assumption that every market requires a completely separate recipe.
When specialist development support is useful
External food R&D support can be valuable when a project involves several linked problems: nutritional reformulation, difficult ingredient interactions, shelf-life uncertainty, scale-up risk or a need to move quickly from concept to manufacturer-ready documentation.
A specialist team can help define the product brief, screen ingredients, build prototypes, organise sensory work, investigate stability, review processing conditions and prepare a more complete technical handover for manufacturing. The most useful support is not simply a new ingredient list. It connects formula, process, testing, cost and regulatory considerations so that improvements in one area do not create hidden failures elsewhere.
Foodsure can support businesses working through formulation, product development, optimisation and commercialisation decisions where the product must satisfy both consumer expectations and production realities. A well-structured development programme gives the team clearer evidence for deciding whether to refine the current formula, change the process, revise the product brief or proceed to pilot manufacturing.
Conclusion
Effective food recipe formulation brings several disciplines into one development decision. Taste and texture must work alongside nutrition. Shelf life depends on the formula, process and pack. Cost includes more than raw ingredients. A kitchen prototype must be tested against commercial equipment, and a product intended for international sale must be reviewed for market-specific labelling, sourcing and compliance requirements.
The strongest formulas are built around clear targets, functional ingredient knowledge, controlled trials and evidence from sensory, analytical and shelf-life testing. When these elements are addressed early, reformulation becomes more purposeful and scale-up carries fewer surprises. Professional food R&D support can help turn that structured approach into a repeatable, commercially viable product.
Frequently Asked Questions
What is food recipe formulation?
Food recipe formulation is the structured process of selecting, combining and optimising ingredients to create a product that meets targets for taste, texture, nutrition, safety, shelf life, manufacturability and cost. It also considers processing, packaging, labelling and consistency between production batches.
What factors should be balanced during recipe formulation?
Key factors include flavour, aroma, texture, nutritional value, ingredient functionality, food safety, shelf life, production requirements, regulatory compliance, sustainability and total product cost. The priority given to each factor depends on the product brief and intended market.
How do formulators balance taste and nutrition?
Formulators use ingredient substitutions, portion control, flavour enhancement, sensory testing and iterative prototyping to improve nutritional value without compromising flavour, texture or consumer acceptance. They also assess how changes to sugar, salt, fat, protein or fibre affect the whole product system.
How is recipe cost calculated?
Recipe cost is calculated by multiplying the required quantity of each ingredient by its unit price, then adding packaging, labour, processing, waste, quality control and other manufacturing expenses. Yield and production losses should be included when calculating the cost per finished unit.
How can food recipe formulation improve shelf life?
Shelf life can be improved through control of moisture, pH, oxygen exposure, water activity, processing conditions, packaging, preservatives, antioxidants and storage temperature. The final shelf-life claim should be supported by testing under realistic storage and distribution conditions.
Why is sensory testing important in food product development?
Sensory testing measures how consumers perceive flavour, aroma, appearance, mouthfeel and overall liking. It helps teams make evidence-based formulation decisions and identify whether a nutritional, ingredient or process change affects acceptance.
What is the difference between a kitchen recipe and a commercial formula?
A kitchen recipe describes how to make a small batch, while a commercial formula must be repeatable at scale and supported by defined processing, quality and safety controls. Commercial development also includes costing, packaging, shelf-life validation and manufacturing documentation.
How long does food shelf-life testing take?
The time required depends on the product, intended shelf life, storage conditions and testing plan. Testing may include real-time studies, accelerated assessments where appropriate, microbiological analysis and sensory or physical checks at planned intervals.
Can one food formula be sold in multiple international markets?
Yes, a common base formula can be practical when ingredient permissions, supply, sensory expectations, labelling and processing conditions are sufficiently aligned. Market-specific reformulation may be needed when regulations, certification requirements, climate exposure or consumer expectations differ significantly.
When should a business seek professional food formulation support?
Professional support is useful when a product must meet several competing targets, such as improved nutrition, extended shelf life, lower cost, a specific claim or reliable large-scale production. Specialist input can help connect formulation, testing, process design and commercial manufacturing requirements.